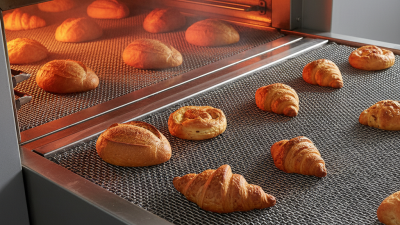
Choosing reliable Furnace Mesh Belt manufacturers requires more than comparing prices or browsing polished product pages. Global buyers need belts that match furnace temperature, atmosphere, load weight, and production speed. A small mismatch can cause distortion, uneven heating, or unplanned downtime.
This guide examines manufacturers through practical purchasing criteria. These include alloy selection, wire diameter, mesh opening, belt construction, edge design, and joining methods. It also considers manufacturing experience, inspection procedures, export capability, and technical support after delivery. Details matter. A belt designed for bright annealing may not suit carburizing, sintering, or heat treatment with heavy components.
Experienced suppliers should explain how their belts perform under repeated thermal cycling. They should provide material certificates, dimensional records, and clear operating recommendations. Traceable testing adds confidence, especially when equipment operates continuously across different regions. Fit matters. The correct belt must also match sprockets, furnace width, tension systems, and cleaning practices.
The manufacturers discussed here serve different industries and purchasing needs. Some specialize in high-temperature alloys, while others focus on custom weaving, rapid production, or large export orders. No supplier is perfect. Lead times may change, and published service life can depend heavily on furnace conditions. That limitation deserves attention.
Careful buyers should request drawings, sample specifications, references, and realistic warranty terms before placing an order. Site conditions should be shared honestly. Testing reveals gaps. A dependable manufacturer does not merely sell a Furnace Mesh Belt; it helps reduce operational risk through measurable engineering support.
Furnace mesh belts support continuous heating, sintering, brazing, and heat treatment. Their design affects product quality, energy use, and maintenance time. Common types include balanced weave, chain edge, rod-reinforced, and conveyor belts with welded links. Each structure handles different loads, temperatures, and product shapes. A balanced weave offers smooth movement for small components. Heavy-duty belts suit cast parts, fasteners, and dense ceramic products.
Material selection requires practical temperature data. Stainless steel is widely used for oxidation resistance and stable dimensions. High-temperature alloys perform better in demanding furnace zones. Nickel-based materials can resist severe heat, but they increase purchasing costs. Some applications need carbon steel for lower-temperature processing. That choice may fail after repeated thermal cycling. Measure operating temperature, atmosphere, load weight, and belt speed before ordering. Applications include powder metallurgy, electronics, food-grade baking, glass processing, and automotive heat treatment.
Tips: Ask for a sample drawing and load calculation. Check edge welds, pitch accuracy, and belt flatness. Confirm spare-part availability and inspection records. A reliable manufacturer should explain material limits clearly. Do not select only by price. I have seen a cheaper belt create tracking problems within weeks. Still, every furnace behaves differently, so field testing remains important. Small adjustments in tension can prevent rubbing, vibration, and uneven heating.
Typical continuous operating-temperature capability of commonly used furnace mesh belt materials. Actual service limits depend on atmosphere, load, belt construction, tension, and heating-cycle conditions.
Commonly used for general heat treatment, drying, annealing, and conveying applications at moderate temperatures.
Selected where improved corrosion resistance is needed, including food-processing and chemically demanding furnace environments.
Designed for high-temperature oxidation resistance in sintering, brazing, forging, and heat-treatment equipment.
Used for demanding high-temperature furnace conveyors, carburizing lines, and applications exposed to oxidation or thermal cycling.
Temperature figures are typical approximate continuous-service ratings for the listed alloys in suitable oxidizing conditions, not guaranteed belt operating limits. Belt selection should be confirmed against the furnace atmosphere, belt mesh design, load, speed, and required working life.
Top Furnace Mesh Belt Manufacturers for Global Buyers
Key Factors for Evaluating Furnace Mesh Belt Manufacturers
Selecting a furnace mesh belt manufacturer requires more than comparing prices. Check its experience with your furnace temperature, atmosphere, product weight, and belt speed. A supplier should explain how alloy selection affects oxidation, creep, and service life. Ask for production records from similar heat-treatment applications. Practical experience matters.
Inspect the belt closely. Welds should be even, with no sharp edges or open joints. Mesh openings must remain consistent across the full width. Ask how the manufacturer controls belt flatness, pitch, and edge alignment. Request material certificates, dimensional reports, and documented load tests. These details support reliable purchasing decisions.
Communication also reveals technical competence. A dependable manufacturer confirms furnace drawings before production. It should discuss sprocket compatibility, tensioning, tracking, and replacement procedures. Clear warranty terms and responsive after-sales support reduce operational risk. References from comparable factories are useful, but they should be verified rather than accepted blindly.
A perfect belt rarely exists. Some suppliers may provide strong material but weak documentation. Others may promise long service life without testing evidence. This is where buyers must slow down. Compare measurable data, not confident language. Consider maintenance access, delivery consistency, and the cost of unexpected shutdowns. The cheapest quotation can become expensive after repeated adjustments, premature stretching, or uneven product heating.
Leading manufacturer profiles now extend beyond weaving capacity. Integrated producers control wire drawing, heat treatment, welding, and belt testing in one facility. Specialist manufacturers often focus on balanced weaves, edge reinforcement, and high-temperature alloys. This matters because furnace belts face oxidation, thermal cycling, abrasion, and uneven loading. The International Energy Agency reports that industry uses about 37% of global final energy, making belt stability relevant to furnace efficiency and production continuity.
Reliable suppliers provide material certificates, tensile data, weld inspection records, and dimensional reports. Buyers should request evidence under ISO 9001 systems and, where applicable, EN 10204 3.1 documentation. A useful profile includes alloy grade, wire diameter, pitch, belt width, maximum operating temperature, and replacement support. Some manufacturers also provide site measurements and trial sections before full production. That practical step can prevent costly fit errors.
Global supply capability is more than export coverage. It includes regional inventory, multilingual technical service, protective packaging, and clear lead-time control. The World Bank’s Logistics Performance Index shows that customs quality and shipment reliability vary widely between markets. Suppliers with local service partners can reduce installation delays. Still, published delivery promises deserve scrutiny. A belt may leave the factory quickly, yet spare components or inspection documents may arrive later. I would compare at least three quotations, but price alone remains a weak selection method. Endurance data should be tested against the buyer’s actual furnace atmosphere, load pattern, and cleaning schedule.
For global buyers, furnace mesh belt quality begins with controlled materials, not attractive catalog photos. Stainless steel grade, wire diameter, and weave pattern should match operating temperature, load, and furnace atmosphere. Reliable manufacturers provide heat certificates, dimensional reports, and batch traceability. They should also document tensile strength, weld quality, belt flatness, and edge finish. These records make supplier comparisons more objective. ISO 9001 certification can support confidence, but it cannot replace process evidence. Ask for recent inspection samples. Not promises alone.
Customization matters when a standard belt cannot maintain stable product movement. Engineers may adjust mesh opening, belt width, chain pitch, rod spacing, and edge construction. The right design reduces sagging, marking, and uneven heating. However, more customization creates more variables. A wider belt may need stronger supports and tighter tension control. A smaller opening may improve product support but restrict gas circulation. Buyers should share load weight, furnace length, speed, temperature profile, and atmosphere details before approving drawings. One missed operating condition can distort an otherwise careful design.
A dependable production process usually includes wire preparation, mesh forming, welding, edge assembly, heat treatment, cleaning, and final testing. Critical dimensions need checks during production, not only before shipment. Trial running should examine tracking, joint smoothness, belt tension, and thermal deformation. Packaging also deserves attention, especially for long ocean transport. Manufacturers with technical staff can explain failure causes and recommend maintenance intervals. Still, no checklist is flawless. Field feedback may reveal wear that laboratory tests missed. Global buyers should review service records, replacement-part access, and response times before placing a large order.
| Furnace Belt Category | Common Material Options | Typical Continuous Service Range | Mesh and Edge Construction | Applicable Quality References | Common Customization Variables | Typical Production Process | Recommended Buyer Inspection Points |
|---|---|---|---|---|---|---|---|
| Stainless Steel Conveyor Mesh Belt | 304 stainless steel for general heat-treatment applications; 316 or 316L where improved corrosion resistance is required. | Usually selected for applications up to approximately 800°C, subject to atmosphere, load, belt design, and exposure time. | Balanced weave, chain-edge, welded-edge, or rod-reinforced construction. Available with sprocket-driven or friction-driven designs. | Material certificates based on ASTM A580/A580M or EN 10204 inspection documentation; dimensional control under an ISO 9001 quality system. | Wire diameter, mesh opening, belt width, overall length, edge style, cross-rod pitch, drive method, and allowable load. | Wire drawing, straightening, weaving or forming, edge assembly, welding, heat treatment when required, leveling, and final dimensional inspection. | Verify material grade, wire diameter, mesh opening, belt width, weld quality, belt tracking, joint design, and certificate traceability. |
| High-Temperature Alloy Mesh Belt | Heat-resistant alloys such as 310/310S stainless steel, nickel-chromium alloys, or other furnace-grade alloys selected for the atmosphere and temperature. | Commonly specified for approximately 900–1,150°C service, depending on alloy selection, atmosphere, tension, and thermal cycling. | Balanced weave, compound balanced weave, reinforced rod structure, or heavy-duty chain-edge construction for high-temperature loads. | Applicable alloy material specifications, EN 10204 certificate levels, ASTM or EN chemical analysis, and documented weld inspection. | Alloy grade, wire size, belt pitch, support structure, edge reinforcement, belt length, and thermal-expansion allowance. | Alloy wire preparation, precision forming, controlled weaving, resistance or TIG welding where applicable, heat conditioning, leveling, and load testing. | Check alloy chemistry, oxidation resistance requirements, weld penetration, thermal expansion allowance, belt sag, and furnace-atmosphere compatibility. |
| Balanced Weave Furnace Belt | 304, 316, 314, 310/310S stainless steel, or nickel-based alloys according to the operating environment. | Often used from moderate-temperature drying and sintering duties to high-temperature heat treatment; the actual limit depends on material and design. | Alternating left- and right-hand spirals connected by straight rods. The structure provides good stability and relatively smooth product conveying. | ISO 9001 quality procedures, material certificates, dimensional inspection records, and customer-approved drawings. | Spiral pitch, rod diameter, mesh opening, belt width, chain spacing, edge type, and product-support surface. | Spiral forming, rod insertion, edge preparation, welding or pinning, belt stretching, flattening, and inspection against approved drawings. | Inspect mesh uniformity, lateral stability, joint flexibility, edge alignment, flatness, and effective conveying width. |
| Compound Balanced Weave Belt | Heat-resistant stainless steels and nickel-based alloys for applications requiring a dense, stable conveying surface. | Typically chosen for elevated-temperature applications where reduced product marking and improved support are important. | Multiple spirals and rods create a tighter surface than standard balanced weave designs, supporting small or delicate parts. | Material traceability, approved engineering drawings, weld inspection, dimensional inspection, and process documentation under ISO 9001 procedures. | Surface density, wire diameter, pitch, belt width, edge construction, drive arrangement, and product-contact finish. | Precision spiral forming, multi-stage assembly, rod insertion, edge welding, tensioning, leveling, and trial fitting with the furnace drive system. | Confirm product support, open-area percentage, belt flexibility, surface flatness, edge weld strength, and compatibility with sprockets. |
| Rod-Reinforced Heavy-Duty Belt | 304/316 stainless steel for general service; 310/310S or heat-resistant alloys for higher-temperature applications. | Selected for heavy loads, impact-prone products, and continuous furnace lines; temperature capability follows the selected alloy. | Thicker cross rods, reinforced edges, and larger support components improve load distribution and resistance to deformation. | Material certificates, weld procedure records, load-test documentation, dimensional inspection, and documented corrective-action procedures. | Rod diameter, rod spacing, belt thickness, reinforcement bars, edge chains, flight attachments, and rated working load. | Rod cutting, forming, mesh assembly, controlled welding, reinforcement installation, belt tensioning, load simulation, and final inspection. | Review working-load calculations, rod straightness, weld strength, chain pitch, belt mass, drive torque, and emergency-stop behavior. |
| Chain-Edge Furnace Belt | Stainless steel or heat-resistant alloy mesh combined with corrosion-resistant or heat-resistant side chains. | Used across a broad range of continuous furnaces; the chain, mesh, atmosphere, and operating temperature must be evaluated together. | Side chains provide positive drive and tracking. The mesh can be balanced weave, compound balanced weave, or rod-supported. | Chain and mesh material certificates, pitch measurement, weld inspection, ISO 9001 process records, and functional test reports. | Chain pitch, sprocket size, belt width, mesh type, cross-rod attachment, edge clearance, and drive configuration. | Chain preparation, mesh assembly, rod-to-chain attachment, welding, pitch calibration, sprocket trial fitting, and tracking verification. | Check chain pitch consistency, sprocket engagement, lateral tracking, side clearance, weld integrity, and thermal-growth compensation. |
| Perforated Plate or Slat Furnace Conveyor | Heat-resistant stainless steel plate, perforated sheet, or formed slats selected for product support and airflow requirements. | Operating temperature is determined by the plate or slat alloy, thickness, furnace atmosphere, load, and support spacing. | Perforated panels or overlapping slats can provide a more continuous conveying surface and controlled airflow. | Sheet or plate material certificates, dimensional tolerances, surface-finish records, weld inspection, and approved fabrication drawings. | Perforation pattern, open area, plate thickness, slat pitch, side guides, flights, belt width, and product-contact finish. | Sheet cutting, punching or laser processing, forming, edge preparation, welding, assembly, leveling, and functional trial inspection. | Verify open area, panel flatness, edge smoothness, airflow distribution, load capacity, thermal distortion, and cleaning access. |
| Custom Furnace Mesh Belt Assembly | Material selected after reviewing furnace temperature, atmosphere, product chemistry, load, belt speed, and maintenance conditions. | There is no universal temperature rating; the design should be validated against the alloy datasheet and actual furnace conditions. | May combine mesh, rods, chains, flights, side plates, trays, crossbars, or special product-positioning components. | Buyer-approved drawings, material traceability, inspection and test plans, weld procedures, dimensional reports, and performance records. | All belt geometry, drive interface, product handling, atmosphere openings, expansion allowance, cleaning method, and spare-part requirements. | Application review, engineering design, prototype or sample approval, controlled fabrication, trial assembly, load testing, and final quality release. | Approve drawings before production; verify critical dimensions, material grades, drive compatibility, thermal clearance, documentation, and installation instructions. |
Selecting the right furnace mesh belt supplier requires more than comparing prices. The World Steel Association reported about 1.88 billion tonnes of crude steel production in 2023, showing the scale of heat-treatment demand. Yet high volume does not guarantee reliable belt quality. Buyers should examine wire composition, mesh opening, belt thickness, edge construction, and rated operating temperature. Ask for material certificates and traceability records.
A capable supplier should provide test data for tensile strength, belt elongation, weld integrity, and thermal distortion. The U.S. Department of Energy’s Industrial Decarbonization Roadmap identifies process heating as a major industrial energy concern, so belt design also affects energy efficiency. A belt that tracks poorly may increase furnace losses and maintenance hours. Request drawings, load calculations, and references from similar atmospheres, temperatures, and product weights. Real evidence matters.
Do not trust a perfect brochure.
During supplier audits, inspect welding consistency under magnification and review replacement lead times. ISO quality certification can support process control, but it cannot replace production samples or independent verification. Published market data may use different definitions, which makes direct comparisons imperfect. That limitation deserves attention. A low-cost belt may appear attractive until downtime, rejected parts, and emergency freight are included. Buyers should run a sample trial, measure belt sag after thermal cycling, and record actual service life. The strongest supplier is not always the largest; it is the one that explains limitations clearly and supports decisions with measurable evidence.